Choosing the Right Mud Recycling System Screen for Operational Success
In the demanding world of drilling, downtime is not just an inconvenience; it is a significant financial hemorrhage. Operators often face the critical challenge of premature equipment failure or screen clogging due to unique rock formations, which directly impacts the efficiency of solids control. The key to maintaining continuous operations lies in selecting a Mud Recycling System Screen that is not merely a spare part, but a scientifically engineered component capable of withstanding harsh environmental variables.
Hebei Fangte Petroleum Machinery Manufacturing Co., Ltd. addresses these precise operational pain points by integrating over 22 years of R&D and production expertise. Established in 2003, we do not simply supply mesh; we provide complete fluid control solutions tailored to specific drilling conditions. Our commitment to resolving complex filtration issues is evidenced by our recent collaboration with a partner in Xinjiang. By diagnosing their unique operational challenges and deploying our optimized screens, we successfully helped them save more than 150,000 USD in operational costs, proving that the right screen choice is a strategic asset.
Engineering Standards for a High-Performance Mud Recycling System Screen
Achieving optimal wellbore productivity requires a rigorous approach to filtration technology. A standard screen often fails to balance conductance with durability, leading to rapid wear or inefficient fluid recovery. At Hebei Fangte, our manufacturing facility, equipped with over 80 specialized machines, adheres to strict quality protocols. We engineer every Mud Recycling System Screen to match the exact specifications of major global brands, ensuring seamless compatibility and superior separation efficiency.
Our technical team analyzes the specific gravity of drilling fluids and the geological formation to recommend screens that extend equipment lifespan. Below is a breakdown of how our engineering standards compare to general industry expectations.
| Performance Metric | Industry Significance | Our Engineering Standard | Advantage |
|---|---|---|---|
| OEM Compatibility | Ensures fitment without vibration or leakage. | Precision retrofitting for Derrick, Brandt, Swaco, and Kemtron. | Zero modification required; seamless installation reduces setup time. |
| Mesh Durability | Resists tearing under high G-force loads. | High-tensile wire configuration with reinforced backing. | Significantly extended screen life, reducing replacement frequency. |
| Separation Efficiency | Critical for removing solids to protect downstream pumps. | Customized weave patterns for specific rock formations. | Prevents screen blinding and maximizes fluid recovery rates. |
| Filtration Accuracy | Determines the quality of the recycled mud. | API-compliant cut point targeting. | Cleaner mud system leading to improved borehole stability. |
Maximizing ROI with a Custom Mud Recycling System Screen
Procurement decisions in the oil and gas sector are shifting from initial price comparisons to Total Cost of Ownership (TCO) analysis. Investing in a premium Mud Recycling System Screen from Hebei Fangte transforms a consumable expense into a value-generating investment. By utilizing our comprehensive replacement screens, operators can significantly reduce the frequency of maintenance shutdowns. Our capability to produce customized solutions implies that regardless of whether you are using Scomi, FSI, or other systems, the filtration performance is optimized to your specific rig conditions.
With a robust workforce of 50+ employees dedicated to quality optimization, we ensure that every screen dispatched from our Anping County headquarters contributes to enhanced wellbore productivity. The chart below illustrates the comparative operational efficiency and cost savings achieved when utilizing Fangte's engineered screens versus generic market alternatives over a standard drilling project lifecycle.
Related products


Top Selling Products

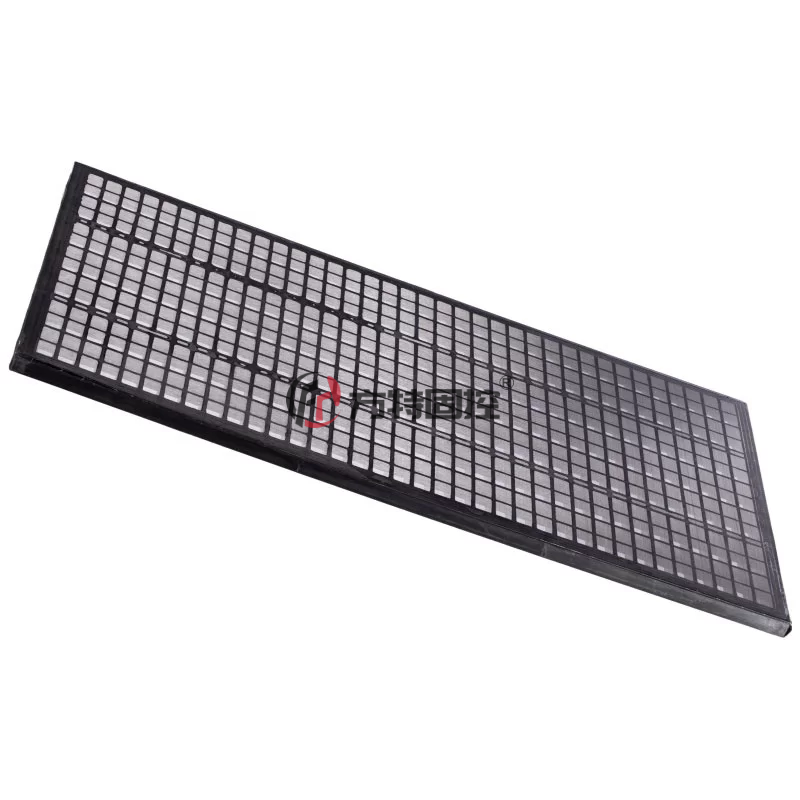



High Performance China drilling shaker screens for Oil Gas

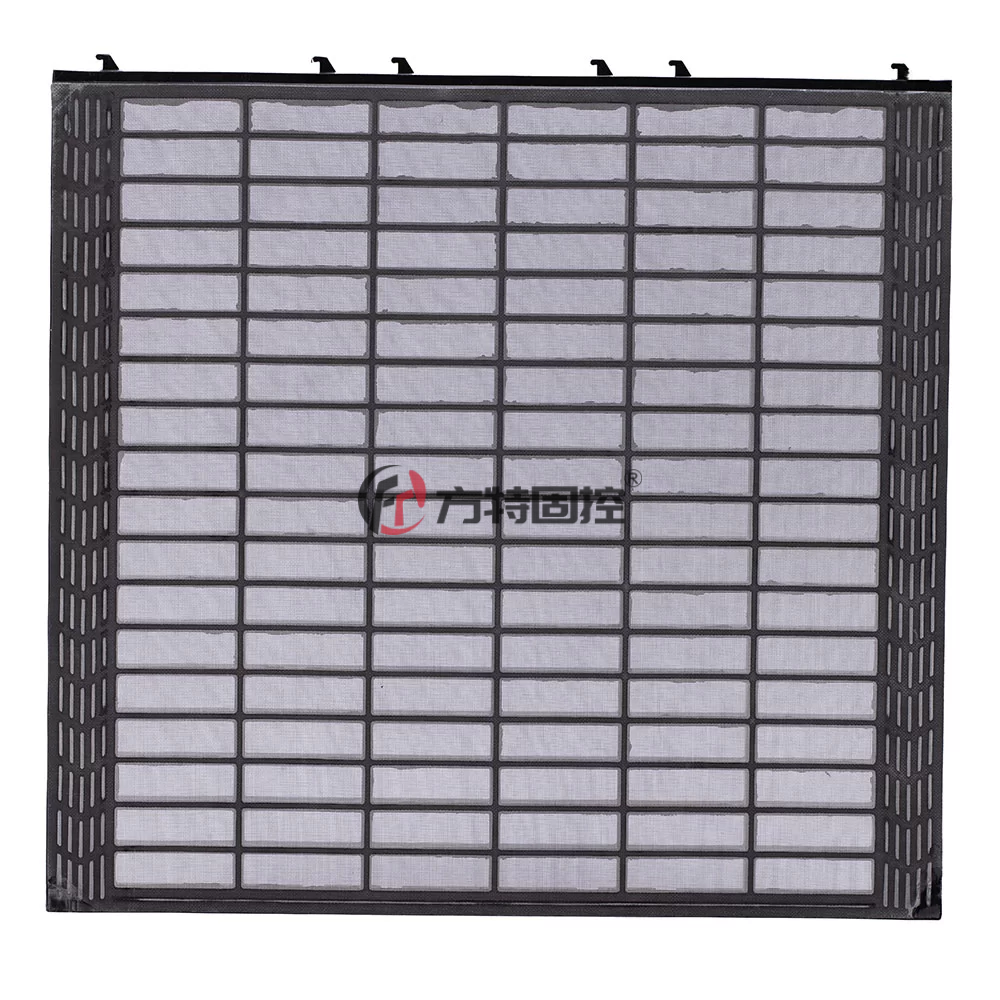
High Performance China drilling shaker screens for FSI 5000

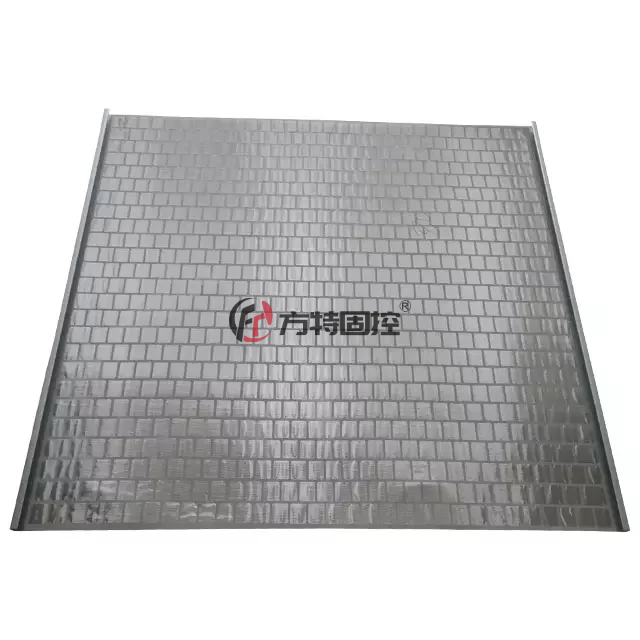
High Performance China oilfield shaker screens for Drilling


